A processing plant in Southeast Asia called us about an RS-485 segment that dropped out several times a shift. Two gateways had already been swapped and the PLC master reflashed before anyone looked at the cable, which is where the problem turned out to be.
Twisted pair cable earns its place in industrial and control systems because two conductors twisted at a controlled lay length collect nearly identical interference, and the receiver subtracts whatever arrives on both. That one mechanism explains its use in fieldbus trunks, 4-20 mA instrument loops, machine-level Ethernet and ordinary interlock wiring. Whether it survives a particular plant comes down to screening, screen bonding and distance from power cabling. The examples running through this article are drawn from projects we have supported, with client details left out.
What Actually Separates a Good Pair From a Bad One

Two specifications distinguish a cable that works from one that looks identical on a cut end. The first is lay length, meaning how tightly the pair is twisted. Inconsistent lay surfaces in the field as crosstalk between pairs on a Fluke test, or as an analogue reading that wanders every time a neighbouring loop switches.
The second is characteristic impedance, and this is where purchase orders go wrong. PROFIBUS DP over RS-485 wants shielded twisted pair near 150 Ω, while PROFIBUS PA runs on pairs of roughly 100 Ω using the Manchester Bus Powered physical layer described in IEC 61158-2. A general purpose control cable with uncontrolled impedance is fine for interlocks and status signals, and it will still produce reflections and CRC errors on a fast bus. Our wider overview of where twisted pair cable is used across different systems maps the rest of the territory.
Fieldbus Trunks and the Real Cost of Sharing a Tray
In that Southeast Asian plant, the answer sat in the route drawings and the site photos, well before we reached the cable schedule. The RS-485 bus connected about twenty field devices to the main PLC, and it ran in the same tray as the output cables from three variable frequency drives, with no divider between them. The installed cable was an unscreened multicore, chosen mainly because the core count was convenient at the time. That combination left the bus wide open to drive noise.
Two site checks confirmed it. The PLC master logged communication errors while every device stayed online, which points at the physical layer, and a continuity check found no usable screen path on that multicore. Termination was already correct at both ends of the trunk, so more gateway swaps and PLC settings work would have led nowhere.
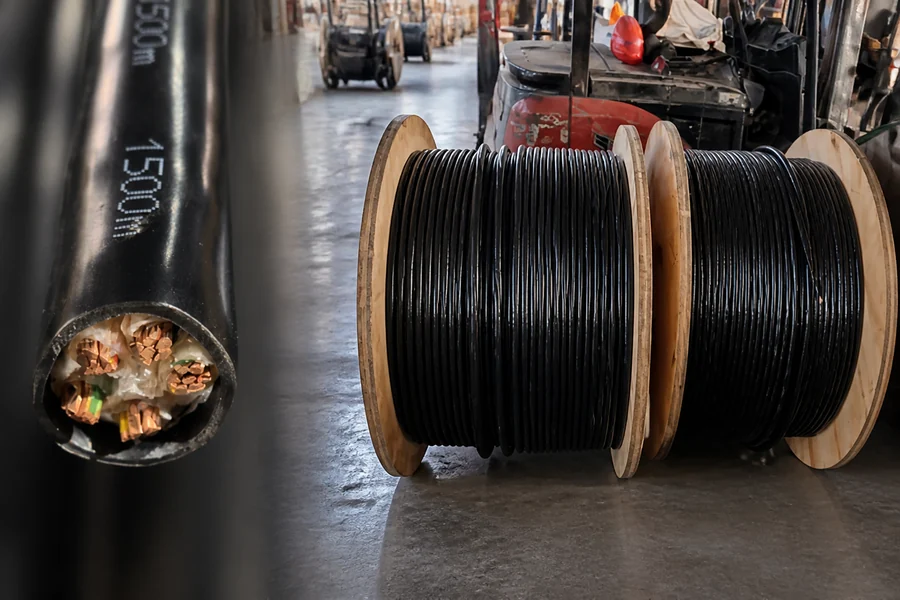
We rebuilt the trunk with shielded twisted-pair fieldbus cable on continuous route-length drums, with no mid-run joints. The segment ran at low speed and was not a PROFIBUS network, so the pair was specified with a defined characteristic impedance matched to that transceiver and route length. For the panel wiring near the drive cabinets we supplied CY braid screened control cable, the international equivalent of KVVP, carrying a tinned copper braid at a minimum of 85% optical coverage. The contractor fitted a steel divider and lifted the bus to the upper tier, and screen bonding followed the device vendor's grounding instructions and the site equipotential bonding design. Communication has been stable since.
The takeaway carries beyond this plant. Where a signal cable passes a drive cabinet, shielding, earthing and separation deserve a look before anyone changes devices or upsizes conductors, because a larger conductor helps with voltage drop and does nothing for bus noise.
| Network | Pair specification we quote against | Distance and speed behaviour | Segment limit |
|---|---|---|---|
| PROFIBUS DP (RS-485) | Shielded twisted pair, approximately 150 Ω | Around 1200 m at 9.6 kbit/s, falling to roughly 100 m in the 3 to 12 Mbit/s range | 32 stations per segment without a repeater |
| PROFIBUS PA (MBP) | Shielded twisted pair, approximately 100 Ω | Fixed 31.25 kbit/s, with power and signal on the same pair | Suited to intrinsically safe areas |
| Industrial Ethernet | Cat5e to Cat7, foil or braid screened in high noise areas | Bandwidth sets the category, and channel length is fixed by the cabling standard applied | Per the design standard named on the project |
PROFIBUS figures reflect the RS-485 and MBP physical layers published by PROFIBUS & PROFINET International and IEC 61158-2:2023, and earlier editions differ in detail. Screen bonding on a PROFIBUS network is its own topic, because the published assembly guidance asks for the screen to be tied into the equipotential bonding system at each station and again at the cabinet entry, using a large contact area. Vendor documentation governs on any specific project.
Instrumentation Loops and the Multipair Screening Decision
When several 4-20 mA loops share one multipair cable, the screening structure matters more than many schedules show. An overall screen protects the cable from external noise, and it does not stop one pair inside the jacket from coupling into another. That is why individually screened pairs are often worth the extra cost on analogue instrument runs.
We saw this clearly on a water treatment plant package. Level and flow readings shifted every time a dosing pump started, then settled again when it stopped, which is the pattern that usually sends people looking at transmitters first. The marshalling cabinet was fed by a twelve-pair cable with a single overall foil screen, and level, flow and control valve loops were all sitting together inside that one sheath. Before replacing the full run, the cheap check was to move one or two affected loops onto individually screened spare pairs and watch whether the drift disappeared, which it did. The final replacement used individually screened pairs under an overall screen, with drain wires bonded at the marshalling cabinet end only.
For water, oil and gas instrumentation tenders, BS 5308 is often named for multipair cable. We quote to that specification when the tender calls it up, and we avoid treating it as a default for every project. The safer approach follows the named standard in the project documents, then chooses the screening structure around the actual signal risk.
Ethernet at Machine and Cabinet Level
Inside a control cabinet, cable category is not always the deciding factor. What matters more is whether the Ethernet cable can resist interference from contactors, switchgear wiring and nearby power circuits. This is exactly the kind of cabinet-level environment where our screened network cables are used.
For these machine and control cabinet drops, our Cat5e, Cat6, Cat6A and Cat7 network cable range includes foil screened and foil plus braid screened options, built on solid bare copper conductors with reference to IEC 61156, TIA/EIA-568 and ISO/IEC 11801. Compared with unscreened cable, these constructions give the signal pair better protection against electromagnetic noise, while proper bonding at the gland plate gives the screen a reliable path to earth.
In metro and industrial control projects, we usually recommend a screened Cat6 for cabinet drops where switches, controllers, contactors and power wiring share a compact enclosure. The cable should still be routed away from the power tier and tested as a channel at handover, because screening works best when the installation supports it.
KVV or KVVP, and Why Buyers Get It Wrong in Both Directions
KVV and KVVP should not be chosen by habit. KVV suits a clean, low-noise route. KVVP belongs where the cable runs near drives, motors, soft starters or large contactors. The mistake is using one type for every route.
For fixed control wiring in panels, trays and conduit away from major noise sources, our unscreened KVV control cable, sold internationally as YY, is usually enough. It uses annealed copper conductors to IEC 60228, with typical configurations from 2 to 37 cores and cross-sections from 0.75 mm² to 10 mm², and higher core counts available on request. It suits interlocks, status signals and general low-energy control circuits.
For routes near drives or heavy switching equipment, a braid screened control cable such as KVVP or CY earns its cost. The screen helps reduce electromagnetic interference. It also adds cost and increases bending radius, so we only recommend it where the route needs protection.
Two details are worth confirming before an order goes to production. The first is spare cores for future changes, because a small modification after commissioning can otherwise mean a new cable run. The second is conductor class, especially for moving parts such as panel doors. A fixed Class 2 conductor is the wrong choice for a cable that bends every day, and a Class 5 fine-stranded construction handles that duty far better.
Installation Errors That Cost More Than the Cable
Four installation habits account for most of the calls we take. Analogue loop screens bonded at both ends, which invites circulating current. Mid-route joints in a screened bus, where every joint is a possible discontinuity in the screen. Missing or duplicated terminating resistors on RS-485 trunks. And standard PVC sheath specified for wash-down or oil-exposed areas where a rubber or oil-resistant sheath belongs.
Separation from power cabling is the fifth, and it does at least as much work as screening. The simplified separation table below is the one most widely quoted from EN 50174-2, and it comes from the earlier editions of that standard. It remains a useful planning reference, and the current 2018 edition works from a cable classification and a calculated minimum separation, so the edition named in the project documents is the one that counts.
| Cable combination | No divider or non-metallic divider | Aluminium divider | Steel divider |
|---|---|---|---|
| Unscreened power and unscreened signal cable | 200 mm | 100 mm | 50 mm |
| Unscreened power and screened signal cable | 50 mm | 20 mm | 5 mm |
| Screened power and unscreened signal cable | 30 mm | 10 mm | 2 mm |
| Screened power and screened signal cable | 0 mm | 0 mm | 0 mm |
These distances come from the older simplified EN 50174-2 table, a European installation standard that applies where a project specifies it, and the values are not a universal rule for every market. North American projects more commonly reference ANSI/TIA-569 and the national electrical code in force, and the numbers differ. Local electrical safety rules take precedence over EMC spacing everywhere. The freely available PROFIBUS and PROFINET installation guidelines go further into earthing, shielding and cable spacing practice than most project documents do.
The Route Review We Run Before Quoting
This is the sequence our engineers work through when a customer sends a cable schedule, and it catches most problems while they are still cheap to fix.
- Signal type on each circuit, meaning fieldbus, analogue loop, Ethernet or plain interlock wiring.
- Required distance and data rate together, because the two trade against each other on the same cable.
- Proximity to drives, motors, soft starters and welding equipment along the actual route.
- Whether the run shares a tray or conduit with power cabling, and whether a divider exists.
- Screen type suited to the noise, and which end the screen is bonded at.
- Terminating resistor arrangement on any bus segment.
- Sheath and temperature suitability for oil, chemicals, wash-down, UV or continuous flexing.
- Acceptance test method agreed before delivery, so handover is not an argument.
If you are preparing an industrial control cable order, contact Anpu Cable with your cable schedule and route drawing before purchasing. We manufacture control and instrumentation cables in our own Wuhan factory, which means we can confirm the right screening structure and custom core configuration before production starts. That helps avoid wrong cable selection, unnecessary cost and delays on project cable orders.
What Production Consistency Buys on Site

Twisted pair cable performance depends on small production details that cannot be checked by eye after delivery. That is why buying from the factory matters. Our routine in-process and final checks cover conductor resistance, insulation thickness, dimensional inspection, screen coverage and high voltage or spark testing, with raw material inspection at the front end and a general inspection before the drum is signed off. Pair-related figures such as lay length and capacitance balance sit on the product datasheet, and we can confirm them against our QC records for a specific build when a project asks for that level of evidence.
Capacitance balance deserves the attention it gets on signal cable. If the two conductors in a pair do not behave evenly, outside noise is no longer received equally on both wires, so the receiver cannot cancel it properly. In the field, this may appear as an instrument reading that shifts when nearby equipment starts or stops, which is the same symptom the water treatment package produced for a different reason.
Flame performance is worth confirming before ordering as well. Our standard PVC control cables meet the IEC 60332-1-2 single cable flame test, and we can supply higher flame-retardant grades such as IEC 60332-3-22 Category A, or low smoke zero halogen constructions, when the project requires them. Our guide to IEC cable standards for construction and fire safety explains how the main test categories relate.
Getting the Route Right Before the Specification
Across the situations above the pattern holds. In each one the cable that failed was a reasonable cable sitting in the wrong electrical environment, and the diagnosis started with the route while the specification sheet came second. Screening choice, screen bonding and distance from power cabling resolved all of them.
Our team has manufactured control, instrumentation and network cable for industrial projects since 1998, from a plant in Wuhan with its own testing laboratory. Core count, cross-section, screening requirement and any named standard are enough for us to return a technical datasheet and a factory price, and we can arrange samples or trial lengths where available before project quantities are committed.
FAQ
Can Cat5 or Cat6 cable be used for RS-485 or Modbus RTU?
Yes, but only when the run and environment make sense. For short, clean runs, a spare twisted pair in Cat5e or Cat6 may work, and long industrial routes near VFDs, motors or power cables should use shielded twisted pair cable specified for the bus impedance and installation conditions.
Should the shield on twisted pair cable be grounded at one end or both?
For most analogue signal and instrumentation cables, one end is the safer default. Bonding both ends can create circulating current if the two ends sit at different earth potentials, while leaving the shield unbonded makes it much less useful. Ethernet, fieldbus and other vendor-specific systems are a separate case, and those should follow the equipment grounding instructions and the site equipotential bonding design.
Can RS-485 cable be run in the same tray as power cable?
It should be avoided where possible. If the route cannot be changed, use proper separation, a metallic divider, shielded twisted pair and careful grounding, especially near VFD output cables where noise is strongest.
Do all 4-20 mA loops need individually screened pairs?
No, not all of them. A single short loop in a clean panel may only need a normal shielded pair, and several analogue loops inside one multipair cable should use individually screened pairs when accuracy matters or when pumps, drives or switching devices are nearby.
What should be checked first when a fieldbus segment keeps dropping out?
Check the cable route before replacing devices. Look at whether the cable runs near drives or motor leads, then confirm termination, shield continuity and screen bonding. Many intermittent RS-485 faults trace back to installation conditions, not the PLC or gateway.
Does a higher Ethernet category solve industrial cabinet noise?
No, category alone does not solve cabinet noise. A correctly bonded screened Cat6 can be more reliable than an unscreened Cat6A beside contactors, because the noise problem is usually shielding and routing, not bandwidth.